Manufacturing decision report
Custom drive system manufacturing: evidence, limits and RFQ decisions
Use the scenario above to organize a supplier discussion. This report explains what the numbers assume, which manufacturing tradeoffs matter, and what evidence to request before approving tooling or series production.
Published by AMRDriveUnit. Created , reviewed . We review this model every six months and after source or method changes. Cost assumptions are editorial scenarios, not measured supplier quotations.
1. Decisions to make before paying for tooling
Price the complete scope
Separate recurring manufacturing cost, tooling allocation and excluded costs. The tool is an internal scenario model, not market pricing.
Specify outcomes separately
A gear tolerance class does not establish assembled backlash, noise or life. Require measured acceptance conditions.
[S1]Validate the environment
Agree immersion, jets, chemicals and continuous thermal duty separately. An IP target alone does not settle these questions.
[S4]Keep safety evidence product-specific
Obtain the exact drive certificate and safety manual; a protocol choice does not establish SIL or PL.
[S5]Plan the market transition
Confirm the supplied-product classification and date of placing on the EU market before choosing the declaration route.
[S6]2. Reproduce the model and understand its limits
All monetary constants and schedule phases are editorial assumptions reviewed on 2026-11-05. No supplier quote dataset or confidence calibration is available. The low/high bands are arithmetic scenario bands. A quoted price can fall outside them. All five numeric inputs use whole numbers; power means mechanical shaft output per drive unit.
| Output | Calculation / basis | Limit and required next step |
|---|---|---|
| Power factor | (shaft power / 750 W)^0.45 | A cost-scaling heuristic; does not size motor torque, gear ratio, bearings or thermal capacity. |
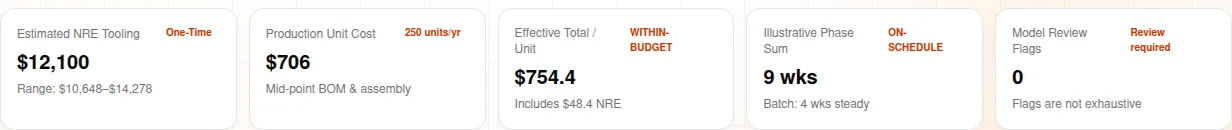
| NRE midpoint | Sum of wheel, housing, gearing, winding and test-fixture allowances. Default: $12,100. | CAD, cavities, tool life and supplier scope can change every allowance. Bands: 0.88× to 1.18× midpoint. |
| Recurring unit midpoint | Sum of seven rounded BOM/process lines after architecture and annual-volume scaling. | Architecture factors: 1.0 / 1.45 / 1.25 / 1.35 / 1.30 in selector order. All seven lines use the same architecture multiplier. |
| Annual-volume factor | Clamp(1.15 − 0.14 × log10(annual volume), 0.62, 1.15) | No batch-price model. Request lot-size quotes and setup fees; annual forecasts are not committed releases. |
| Effective unit cost | Recurring midpoint + NRE midpoint / annual volume, rounded to $0.10. | Annual allocation is not a supplier installment-payment offer. Assumes one year of volume absorbs all NRE; excludes freight, duties, tax, design labor, certification, validation, scrap and warranty reserves. |
| Budget status | Effective cost vs target: within ≤0%; near >0–15%; exceeds >15%. | Status uses the unrounded variance; displayed percentage is rounded. Not a landed-cost comparison. |
| First article | DFM + tooling + prototype + FAI phases. Default: 2 + 2 + 3 + 2 = 9 weeks. | Sequential illustrative phases; tooling weeks model housing only. Motor, tread, gear tooling, procurement and capacity are excluded. Obtain a complete supplier plan. |
The default scenario currently gives $706 recurring cost plus $48.4 NRE allocation = $754.4 effective cost per unit. Compare this with drawing-based quotations on the same scope.
Review flags cover low-volume die tooling, sealed high-power duty, tight schedules, cast-housing precision targets, high-power cost scope and cycloidal architecture mismatches. They are not exhaustive. Zero flags does not validate torque, current, thermal rating, life, safety or supplier capability. Wheel geometry and architecture-specific tooling require separate quotes; the generic factors cannot price every steering mechanism or individual Mecanum roller.
3. Make, buy or commission a custom assembly
Compare qualified alternatives before defaulting to bespoke manufacturing. Custom work can resolve an interface or packaging constraint, but adds change-control and validation obligations. This is a decision framework; it is not a ranking of suppliers.
| Route | Useful when | Tradeoff / evidence to request |
|---|---|---|
| Catalog assembly | A proven torque-speed envelope and mounting arrangement meet the need. | Confirm availability, duty rating and integration evidence; adapt the vehicle only where justified. |
| Semi-custom assembly | The motor/gearing are suitable but the mount, hub or harness differs. | Define the changed interfaces and requalification scope; retain evidence only where still applicable. |
| Custom OEM manufacture | A documented constraint cannot be met by qualified standard parts. | Freeze drawings, tool title, acceptance tests, change authority and commercial scope before tool release. |
| In-house manufacture | Process ownership, equipment and quality capacity support the program. | Include equipment utilization, process qualification, inspection and staffing in the comparison. |
4. Gate the prototype-to-series lifecycle
Release tooling only after critical interfaces are agreed. First-article approval records conformity of a sample; series release also needs a control plan, traceability, deviation handling and a stable process. Tool changes should reopen affected validation gates.
5. Gears and bearings: specify what must be measured
Grade labels describe particular measurements under a named standard and edition. ISO 1328-1 concerns individual cylindrical involute gear flanks; do not use it as a universal table of assembled backlash or acoustic limits. Lead crowning and tip relief need a load-dependent design, not a fixed recipe. [S1]
For a cantilevered wheel, moment M = Fr × x is only the starting point. Load spectrum, bearing spacing, speed, lubrication, fits and temperature are still needed. ISO 281 basic rating life concerns fatigue with a stated reliability basis; wear, corrosion and electrical erosion lie outside that model. No fixed 20,000-hour life follows from choosing a back-to-back bearing pair. [S2]
| Topic | Put in the specification | Verify on the assembly |
|---|---|---|
| Gear geometry | Module, ratio, material, treatment, flank class, edition and measured parameters. | Contact pattern, backlash, loaded torque-speed behavior and agreed noise test. |
| Bearing support | Loads, offsets, speed, duty, temperature, fits and preload method. | Runout, temperature, drag and validation for the actual load spectrum. |
| Tolerance stack | Critical datums and fit stack through gear seats, bearings and housing. | First-article measurement report and disposition of worst-case interference. |
6. Wheel tread: qualify the compound and bonded interface
Specify the exact elastomer and process rather than treating hardness as a complete material specification. Surface preparation, primer, cure, core geometry and storage all affect bond performance. Request compound documentation and loaded rolling tests at the actual speed and duty.
Covestro describes NDI-based Vulkollan as a material family with high dynamic load capacity. That supports evaluating it; it does not establish universal loss-tangent values, a 55°C rolling temperature, or a prescribed peel-force limit for every wheel. Compare DMTA loss-tangent data only at matched temperature, frequency and strain conditions. [S7]
7. Motor winding, balancing and thermal integration
A winding change affects current, speed constant and losses. Agree a measured torque-speed envelope over bus limits and temperature, plus insulation and magnet limits for the selected construction. Mechanical output power alone cannot establish the electrical current or winding temperature.
For rigid rotors, use the ISO 21940-11 family rather than presenting withdrawn ISO 1940-1 as the current reference. Agree speed, grade, correction planes and a balance report. Generic fixed residual-unbalance values do not transfer between rotor designs. [S3]
8. Housing economics, sealing and environmental fit
CNC avoids dedicated casting dies but still needs CAM, workholding and inspection. Casting adds tool investment and may still need finish machining at bearing datums and seal lands. Break-even quantity = incremental tooling cost / verified recurring saving per part. Use lifetime committed units, then add tool maintenance, changes and scrap. No universal 400–700 units/year crossover is supported here.
| Route | Potential benefit | Question before approval |
|---|---|---|
| Billet CNC | Design flexibility without casting dies. | How much setup and machine time is needed, including datum control? |
| HPDC | Shorter casting cycle after qualified tooling. | What are die cost, life, porosity control and finish-machining requirements? |
| Gravity casting | An alternative tooling and material route. | Can the process meet structural and dimensional requirements after machining? |
| Stainless CNC | A candidate where the cleaning environment justifies the alloy. | Which chemicals, surface finish, crevices and thermal limits must be qualified? |
IP67 describes dust-tightness and temporary immersion. It does not automatically qualify water jets or high-pressure chemical washdown. Dry pressure-decay and helium tracer-gas methods are different tests; either needs a defined setup and correlation with qualified assemblies. Seal-track finish, lead, runout and material must be agreed with the seal supplier. [S4]
9. Electronics and safety functions need separate evidence
Specify fieldbus profile, firmware, connector pinout, voltage limits and fault behavior. EtherCAT or CANopen describes communication; neither establishes functional safety. Ask for the specific STO safety manual and certificate, then assess integration assumptions, diagnostics and validation of the full safety function. [S5]
IEC lists an amendment to IEC 61800-5-2 dated 30 October 2026. Confirm the applicable edition and the certified product scope rather than inferring a SIL or PL from this page. Potting or a sealed enclosure does not remove the need to measure heat flow and serviceability.
10. Agree quality gates and compliance responsibilities
| Gate | Evidence to agree | Boundary |
|---|---|---|
| Incoming parts | Material certificates, heat-treatment records and revision traceability. | Certificate type and acceptance criteria depend on the contract and drawing. |
| First article | Ballooned dimensional report, balance report and measured functional results. | Sample conformity does not prove life or series process capability. |
| Qualification | Loaded endurance, thermal, environmental and safety validation plans. | Define samples, conditions and pass criteria; distinguish destructive tests. |
| Per-unit production checks | Identity, wiring, firmware and agreed functional checks with serial records. | Do not label every qualification test as a 100% EOL test. |
| Shipment release | Deviation disposition, inspection records and configuration identification. | Release only to the agreed scope; close outstanding customer approvals. |
As of 2026-11-05, the European Commission gives 20 January 2027 as the general application date for Regulation (EU) 2023/1230. Confirm the supplied-product classification and market-placement date. A drive assembly may require partly completed machinery treatment depending on its scope; the page cannot classify every motor or module automatically. Other applicable legislation must also be assessed. [S6]
11. Illustrative scenarios and failure prevention
These are model demonstrations, not delivered customer cases or measured factory outcomes. Select the same preset above to reproduce the inputs. Monetary figures remain internal scenario assumptions.
AMR Traction Hub (750W / 48V)
Inputs: 250 units/year, 25/lot, billet-cnc-6061.
Process: apply the same NRE, annual-volume and sequential schedule rules.
Model output: $12100 NRE; $754.4/unit including NRE; 9 weeks to first article.
Next: compare a qualified catalog or semi-custom option before committing to custom gearing.
Ultra-Flat Shuttle Drive (400W / 24V)
Inputs: 1500 units/year, 150/lot, hpdc-aluminum-a380.
Process: apply the same NRE, annual-volume and sequential schedule rules.
Model output: $29500 NRE; $637.7/unit including NRE; 16 weeks to first article.
Next: validate the committed lifetime quantity, casting tool title and machining allowance.
Stainless Immersion Target (500W / 48V)
Inputs: 60 units/year, 10/lot, stainless-cnc-304.
Process: apply the same NRE, annual-volume and sequential schedule rules.
Model output: $20000 NRE; $1314.3/unit including NRE; 12 weeks to first article.
Next: qualify chemicals, jets and thermal conditions; IP67 alone does not approve cleanroom washdown.
| Risk | Consequence | Minimum action / alternative |
|---|---|---|
| Misuse of model output or grade labels | An unvalidated assembly is treated as safe or durable. | Get drawing-based analysis and measured qualification; use an already qualified catalog design if suitable. |
| Forecast-only tooling recovery | NRE is spread over units never purchased. | Compare committed lifetime quantities and staged tooling; retain CNC for uncertain pilots. |
| Scene mismatch | A wheel, seal or motor fails outside its tested environment. | Validate floor, cleaning and duty conditions; choose a compound or housing only after matched tests. |
| Tooling and IP lock-in | A later supplier transfer requires unexpected redesign or repurchase. | Define tool title, access, maintenance, transfer and background-IP rights in the contract. |
| Schedule compression | Tool corrections or failed FAI delay the production launch. | Gate the ramp on measured samples; consider a CNC pilot while qualifying hard tooling. |
12. Manufacturing RFQ questions by decision stage
Engineering & DFM
What data is needed for a custom drive manufacturing DFM review?
Provide STEP models, revision-controlled 2D drawings, datum and fit requirements, torque-speed duty cycle, radial and axial loads, wheel offset, bus limits and interfaces. If these are incomplete, request a gap review before accepting a fixed manufacturing quote.
Does DIN Grade 6 guarantee low backlash or a noise limit?
No. Specify the standard and edition, gear geometry and measured flank deviations. Assembled backlash, efficiency and noise require separate acceptance conditions. ISO 1328-1 classifies individual cylindrical gear flanks and cautions against predicting assembled performance directly from loose-gear tolerance classes. See [S1].
[S1]How should lead crowning and tip relief be specified?
Derive flank modifications from gear geometry, deflection, load spectrum and loaded contact analysis. Confirm them by measurement and a loaded test. A fixed micrometre range does not establish an ISO 6336 safety margin or an acoustic result for an unspecified gearbox. See [S1].
[S1]How do overhung moment and bearing preload affect selection?
Record wheel radial load and offset: moment M = Fr × x. The bearing arrangement must also account for axial loads, shock, speed, fits, lubrication and temperature. Agree preload with the bearing supplier; a back-to-back arrangement alone does not establish a fixed life. ISO 281 rating life is a fatigue calculation, not a service-life guarantee. See [S2].
[S2]What should the wheel tread qualification specify?
Agree the exact compound, hardness range, core preparation, bonding system and cure route with the caster. Validate adhesion and loaded rolling endurance after relevant conditioning. A generic peel-force number is not evidence that every tread or core design will survive the duty cycle.
When is low loss-tangent polyurethane worth evaluating?
At sustained speed or heavy cyclic loading, compare loss factor over the relevant temperature, strain and frequency range, then measure tread temperature in a loaded rolling test. Covestro identifies Vulkollan as an NDI-based material with high dynamic load capacity; this does not prove a universal maximum temperature or rule out other compounds. See [S7].
[S7]Does zero-lead plunge-ground shaft finishing guarantee a leak-free seal?
No. Discuss a lead-free seal track, surface finish and hardness with the selected seal supplier. Shaft runout, eccentricity, lubricant, pressure, wear and cleaning conditions also matter. Correlate a production leak test with the qualified assembly rather than adopting an arbitrary universal leak threshold.
Does IP67 cover washdown or establish continuous thermal power?
No. IP67 is a dust-tight and temporary immersion target under IEC 60529, not automatic water-jet or chemical-cleaning approval. Specify cleaning pressure, temperature, chemistry and operating state separately. Validate continuous output in the actual mounting, ambient and duty cycle; this tool does not calculate temperatures. See [S4].
[S4]Tooling & Economics
Are the calculator cost ranges supplier quotations?
No. They are illustrative internal model bands reviewed on 5 November 2026, with no supplier quote dataset behind them. They exclude freight, duties, tax, design labor, certification, validation, scrap and warranty reserves. Get a drawing-based quotation with currency, Incoterm, validity, tooling ownership and payment terms.
At what volume should CNC be replaced by die casting?
Calculate break-even quantity from the incremental tooling investment divided by verified recurring savings per part. Include finish machining, changes, maintenance, scrap and the committed lifetime quantity. There is no universal annual-volume crossover. The model flags HPDC below 500 units only as a prompt to compare quotes.
Does changing batch size change the modeled unit price?
No. This version applies an annual-volume factor to recurring cost. Batch size affects the modeled repeat-lot schedule only. Request a lot-size price matrix, setup charges and release schedule from the supplier before comparing purchase options.
Can catalog parts be combined with custom manufactured parts?
Yes, evaluate retaining a qualified motor or gear stage while customizing the mount, hub or housing. Confirm interface ownership, availability and whether the changes invalidate existing thermal, ingress or safety evidence. Compare the full qualification scope before committing to a bespoke assembly.
Quality & Testing
Which checks should be performed on every unit versus a qualification sample?
Agree a control plan. Per-unit checks can cover identity, firmware, wiring and functional operation; endurance, environmental, destructive bond and full-load qualification need a separate sampling and validation plan. The tables on this page propose discussion topics, not a claim that every listed test is performed on every supplied unit.
Which rotor balancing standard should be referenced?
For rotors with rigid behaviour, discuss ISO 21940-11, which succeeds ISO 1940-1. Agree operating speed, balance grade, correction planes and measurement report. A balance grade does not imply the same residual-unbalance number for every rotor or speed. See [S3].
[S3]What records should accompany first-article samples?
Agree ballooned dimensional reports, material and heat-treatment traceability, assembly revisions, test conditions and measured results. List open deviations and their disposition. First-article approval must not be presented as proof of long-term life or complete robot compliance.
Can a dry leak test replace IP qualification?
A calibrated dry pressure-decay or tracer-gas test can support production screening after correlation with qualified assemblies. The gas, volume, pressure, stabilization, temperature and allowable leakage must be specified. It does not by itself establish an IEC 60529 rating, chemical resistance or seal endurance. See [S4].
[S4]Does selecting EtherCAT and STO establish SIL 3 or PL e?
No. A communication protocol and a checkbox do not establish a safety integrity level. Request the exact hardware and firmware certificate, safety manual, diagnostic assumptions and integration constraints, then validate the complete safety function. IEC 61800-5-2 addresses safety-related drive subsystems; its 2026 amendment is listed in [S5].
[S5]Lead Time & Ramp-Up
Are first-article weeks a promised delivery date?
No. The tool adds illustrative DFM, tooling, prototype and FAI phases. Drawing maturity, material availability, tool iterations, test failures and factory capacity can change the schedule. Get a dated supplier plan with dependencies and acceptance gates before promising a launch date.
How should recurring production delivery be agreed?
Confirm order-release quantities, material buffers, capacity reservation, forecast commitment and shipping terms. The repeat-lot weeks in this tool are internal assumptions and do not include transport, customs or a guarantee of stock.
How should international logistics enter the RFQ?
Request packed dimensions and weight, corrosion protection, handling requirements, shipping mode and Incoterm. Obtain a logistics quote and any relevant transport assessment for the exact shipment. The calculator does not include freight, import charges or packaging qualification.
Who owns tooling, drawings and firmware adaptations?
Agree these rights in writing before payment. Define physical tool title, custody, maintenance, access, transfer cost, background IP and licensed firmware separately. An NDA protects agreed confidentiality; it does not automatically transfer design or tooling ownership.
How does Regulation (EU) 2023/1230 affect a custom drive system?
As reviewed on 5 November 2026, the European Commission states that the Machinery Regulation generally applies from 20 January 2027; the Machinery Directive governs machinery placed on the market before then. Classify the supplied assembly individually. For partly completed machinery under the Regulation, agree incorporation documentation and assembly instructions; the integrator remains responsible for the complete machine assessment. See [S6].
[S6]13. Source ledger and evidence boundaries
Primary-source pages checked on 2026-11-05. Public abstracts establish scope, not all normative acceptance clauses. Use the licensed applicable edition and project drawings for contractual requirements. None of these sources validates this page’s price or schedule assumptions, proves supplier capability, or certifies a product.
- [S1] ISO 1328-1:2013 — gear flank tolerance scope and limitations
Scope: Individual cylindrical gear flank classification; not a universal backlash, noise or surface-finish guarantee.
- [S2] ISO 281:2007 — bearing load ratings and fatigue rating life
Scope: Basic and modified rating-life methods; excludes wear, corrosion and electrical erosion.
- [S3] ISO 21940-11:2016 — balancing rotors with rigid behaviour
Scope: Balance procedures and tolerances; supersedes withdrawn ISO 1940-1. See the listed 2022 amendment.
- [S4] IEC 60529 — enclosure IP classification
Scope: Enclosure classification under specified tests; not chemical compatibility or lifetime evidence.
- [S5] IEC 61800-5-2:2016/AMD1:2026 — drive functional safety
Scope: Amendment published 30 October 2026; confirm the applicable edition and specific drive safety evidence.
- [S6] European Commission — Machinery legislation and transition
Scope: General application from 20 January 2027; assess the product classification and market-placement date.
- [S7] Covestro — Vulkollan material family
Scope: Manufacturer description of NDI-based elastomer properties; no universal rolling temperature or bond-strength threshold.
14. Turn the scenario into a reviewable RFQ
Copy the tool’s brief, paste it into the inquiry message, and add drawing revisions, torque-speed/load data, duty cycle, ambient and cleaning requirements. Agree a secure file-sharing route for CAD. Ask for a scoped quotation and a dated validation plan; response timing and firm pricing depend on complete inputs and supplier review.